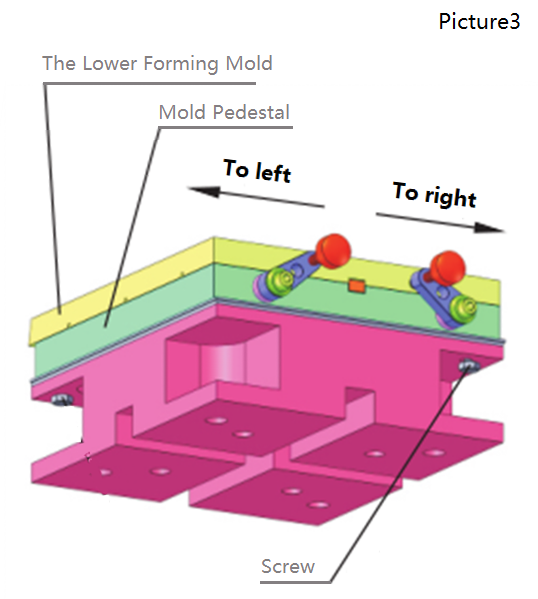
Schematic Diagram: DPH Series Blister Machine Formed Web Parallel Alignment and Calibration SOP
02/24/2019
In the continuous-motion architecture of DPH series equipment, the formed PVC web is advanced by the indexing mechanism into the feeding zone, guided by dedicated linear rails. Absolute parallelism between the formed blister cavities and the guide rail is critical for downstream sealing registration. For a comprehensive overview of our complete equipment capabilities and formats, please refer to our full range of Blister Packaging Machines.
1. Diagnosing Web Tracking Deviation
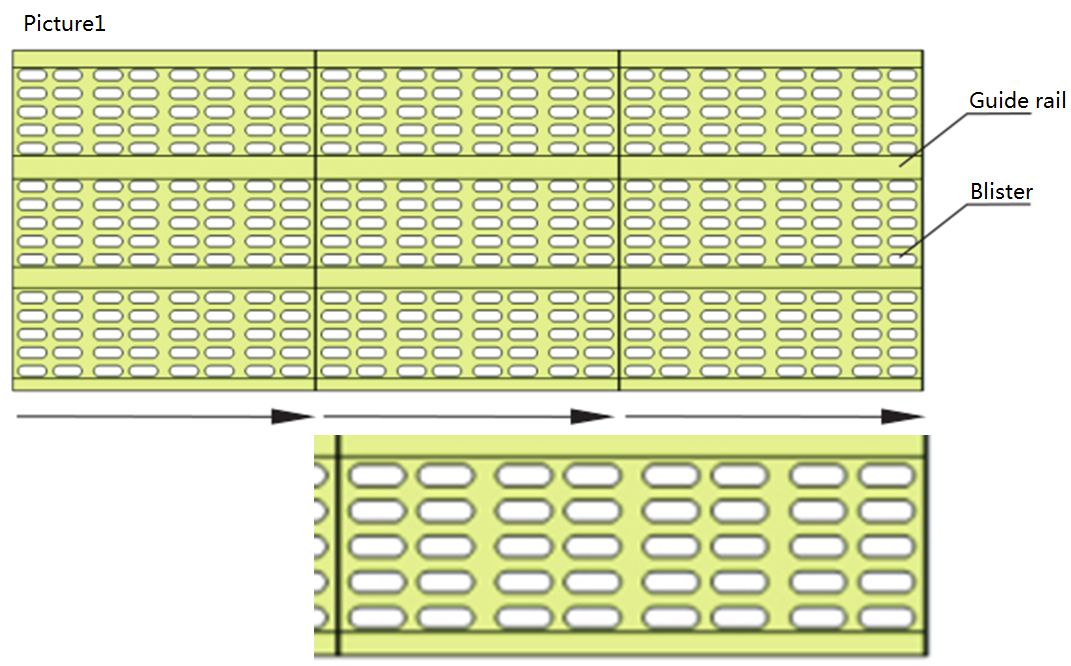
Under optimal conditions, the blister cavities must run strictly parallel to the guide rail (see Figure 1). However, due to mechanical assembly tolerances or operational drift, the web may exhibit a skewed trajectory, inclining to the left or right (see Figure 2). This tracking deviation is typically caused by a misalignment of the lower forming mold, where its longitudinal centerline is no longer perfectly parallel to the guide rail’s centerline.
2. Standard Operating Procedure (SOP): Parallelism Calibration
- Safe Access: Power off the blister machine. Remove the exterior stainless steel protective cover at the forming station to access the lower mold assembly.
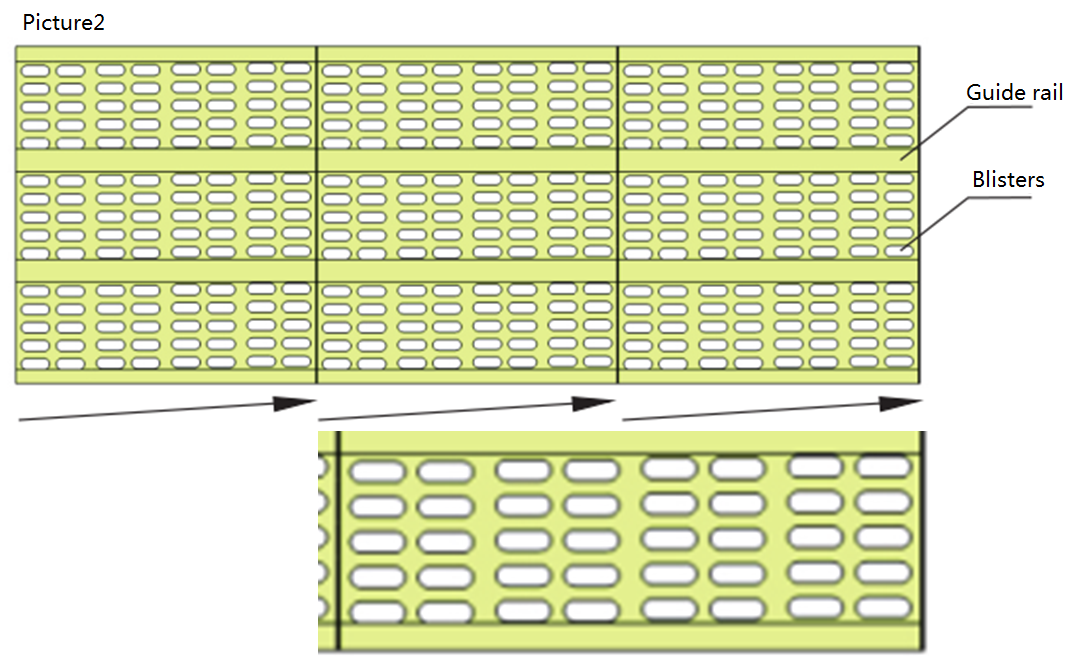
- Mechanical Adjustment: Locate the adjustment screw [3] situated beneath the lower forming mold (see Figure 3). Loosen this screw to free the forming mold pedestal [2]. Based on the observed tracking deviation, execute micro-adjustments by shifting the pedestal slightly to the left or right axis.
- Validation & Securing: Lightly fasten the screw [3]. Power on and inch the machine to form a new web section. Inspect the newly formed blisters against the guide rail. Once absolute parallelism is restored (matching Figure 1), apply final torque to securely lock screw [3] and reinstall the stainless steel cover.