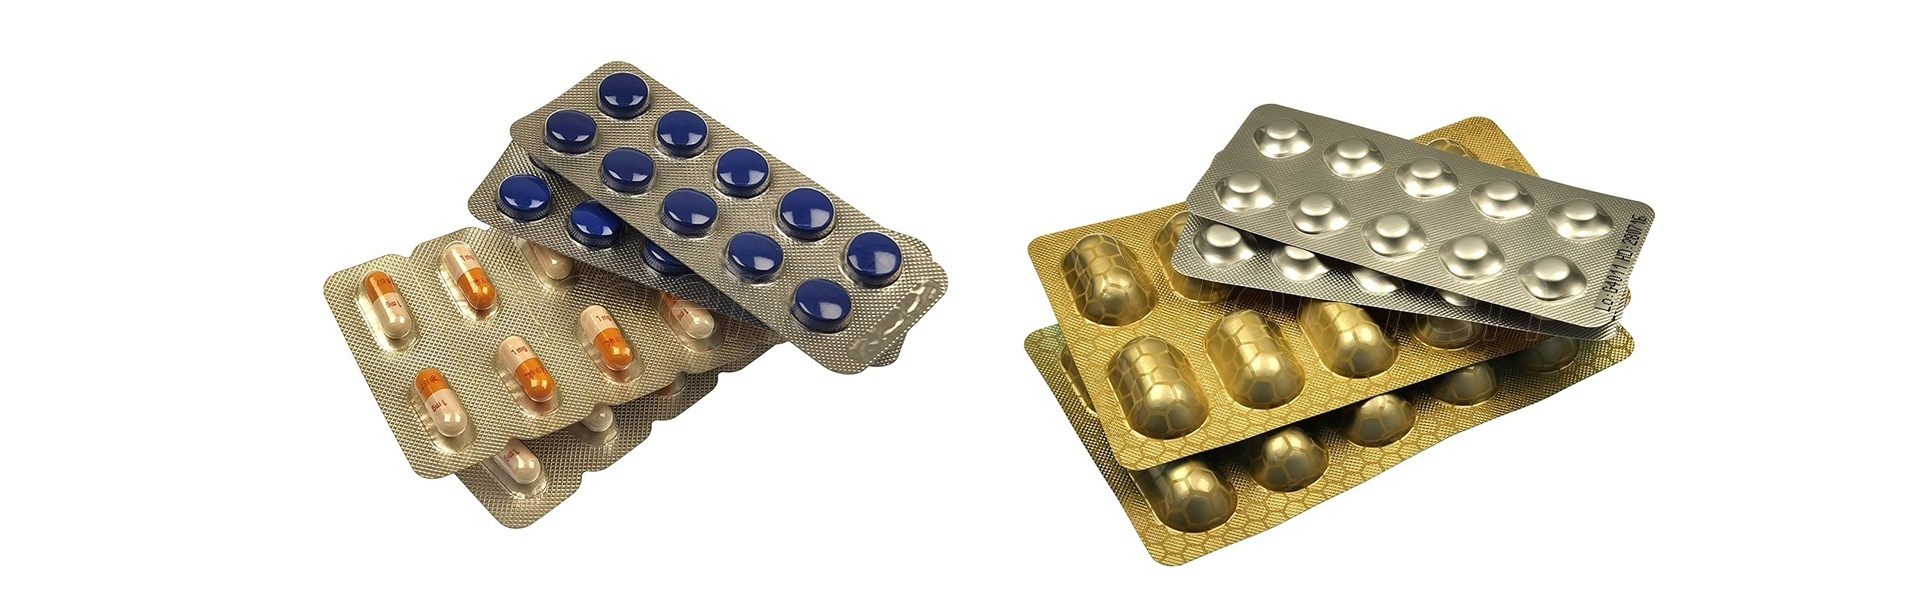
A blister pack is a highly efficient, unit-dose packaging solution widely adopted in the pharmaceutical industry for products such as tablets, capsules, ampoules, vials, and syringes. While also used for consumer goods and cosmetics, its primary value in pharmaceuticals is providing multiple levels of barrier protection based on the drug’s specific characteristics to extend shelf life and ensure reliable tamper-evident security.
A blister pack has two main components: a formed cavity (or pocket) made from thermoformed plastic or cold-formed aluminum film, and a secure lidding material, typically aluminum foil or plastic laminates.
In pharmaceutical applications, these are frequently referred to as push-through packs (PTP). This designation highlights two critical mechanical properties: a flexible, semi-rigid cavity that allows users to easily press the product out, and a specially engineered brittle lidding foil designed to rupture cleanly for effortless dispensing.
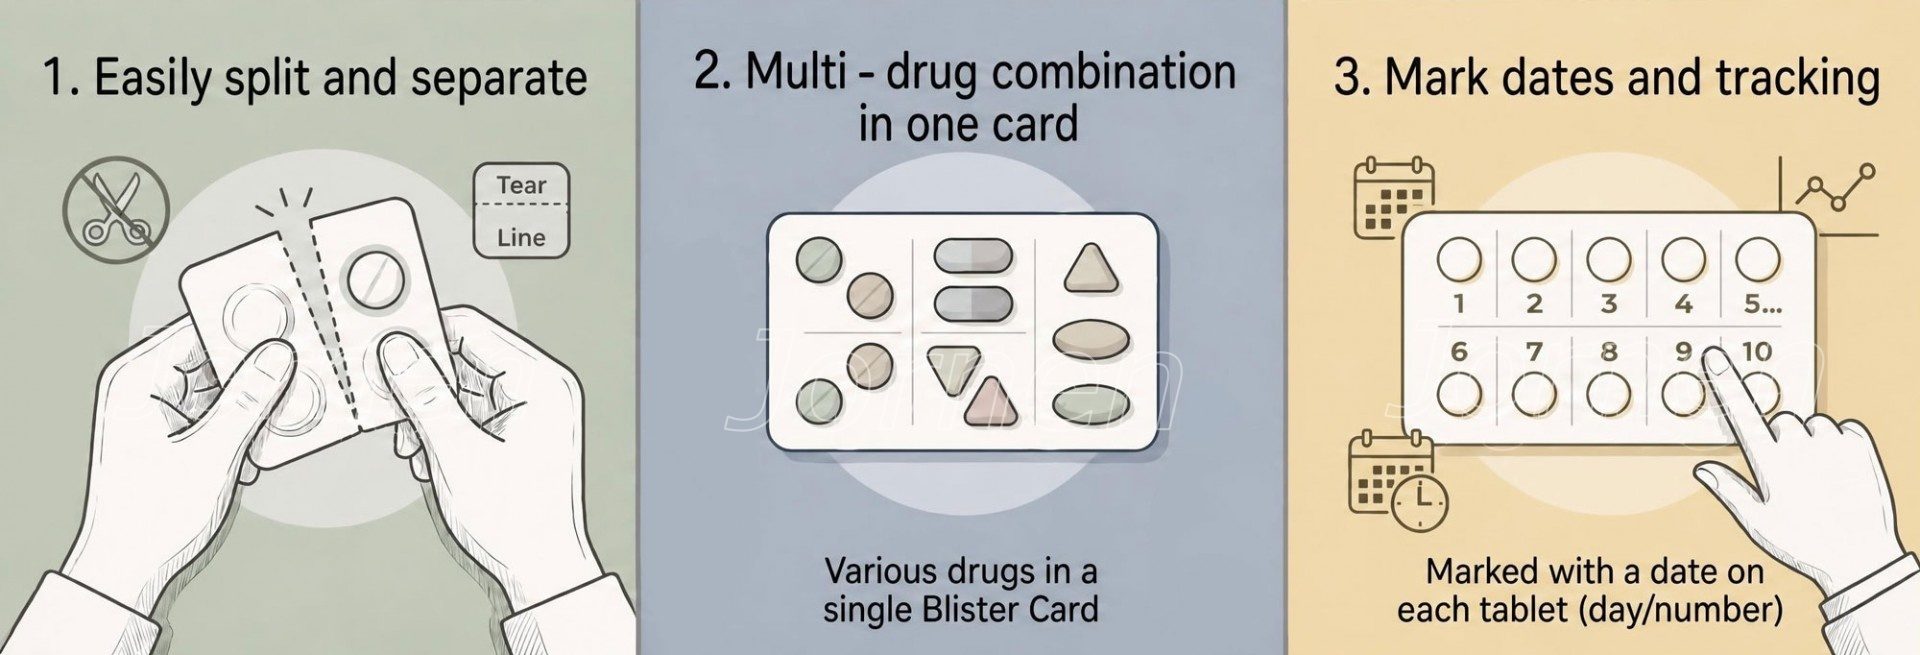
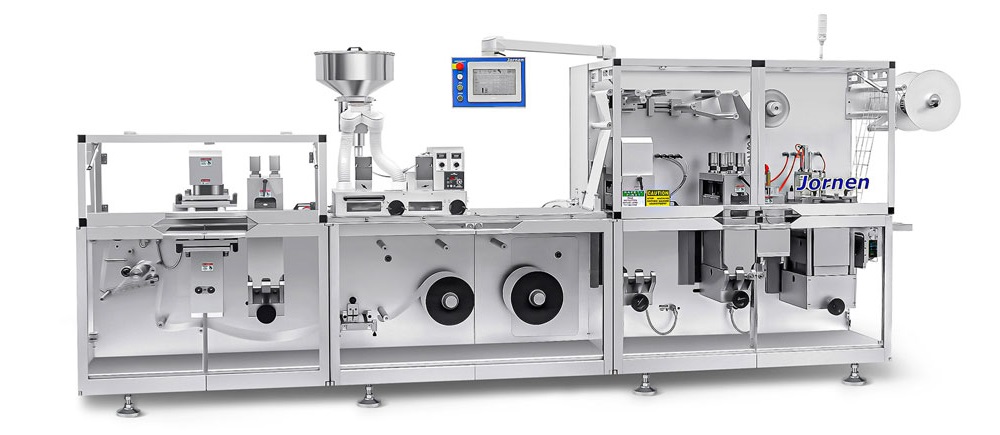
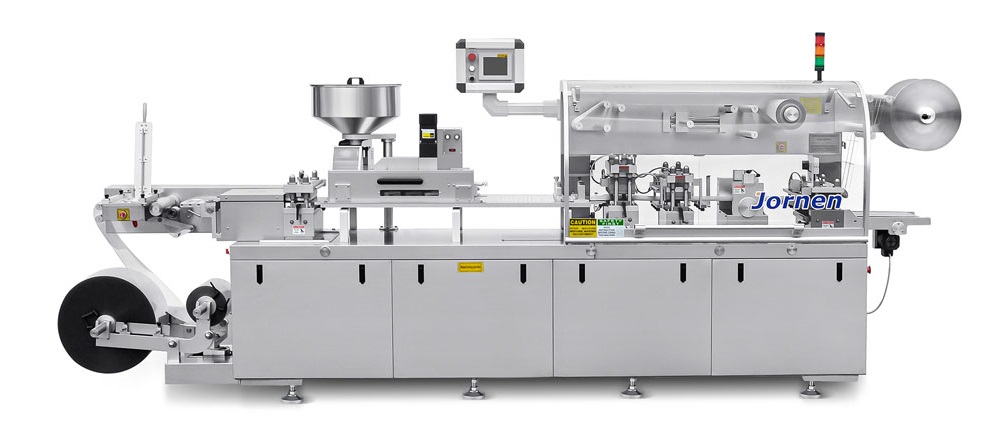
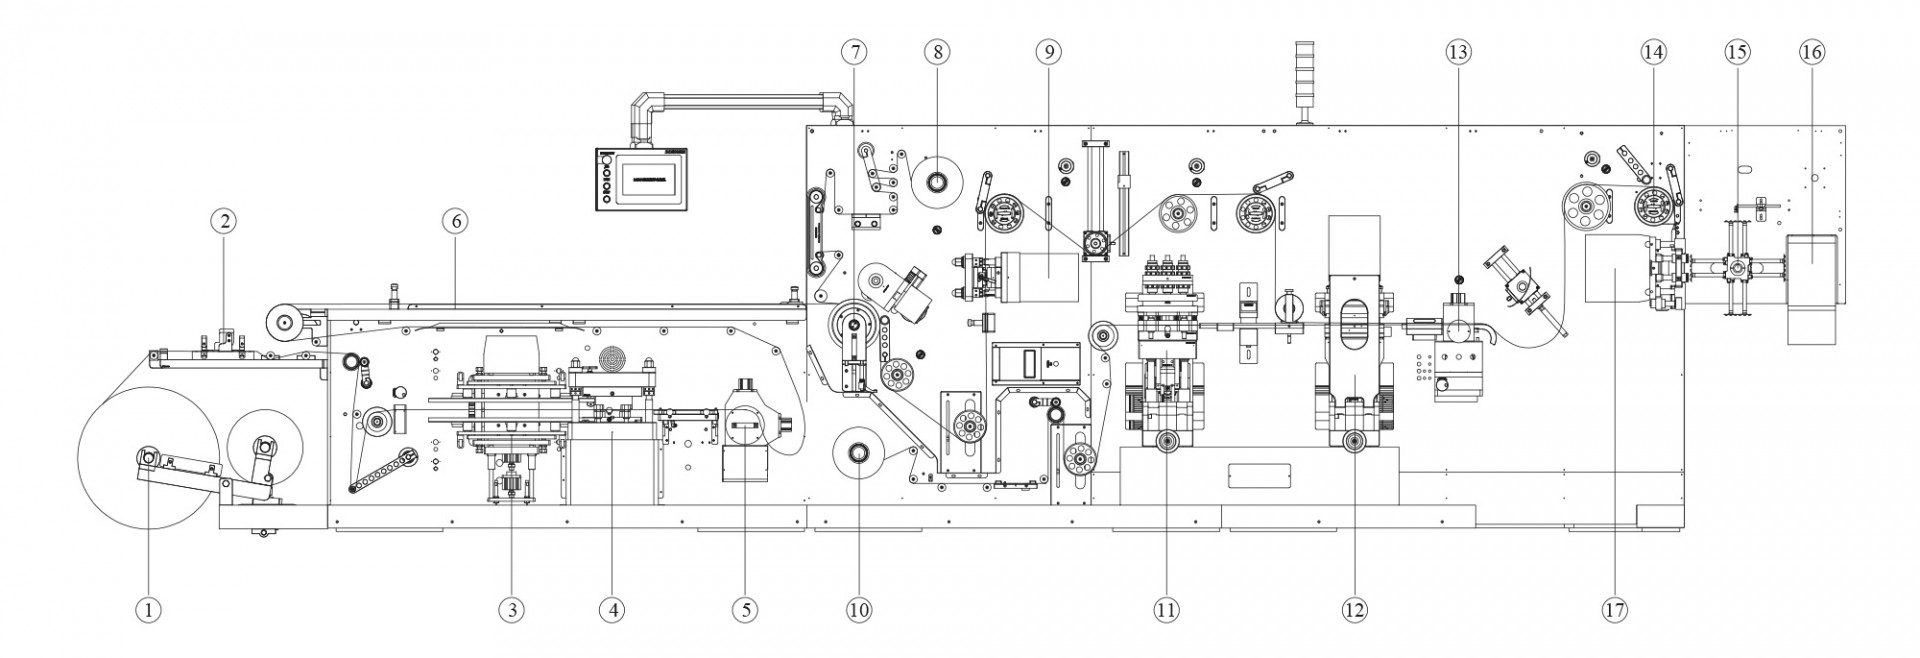
A blister packaging machine is a comprehensive, automated system engineered to execute the complete unit-dose packaging process. The equipment integrates a series of precisely coordinated stations to form, feed product, seal, emboss, perforate, and punch.
Based on their core sealing mechanisms and kinematic principles, these machines fall into two main designs: platen-type (intermittent-motion) and rotary-type (continuous-motion).
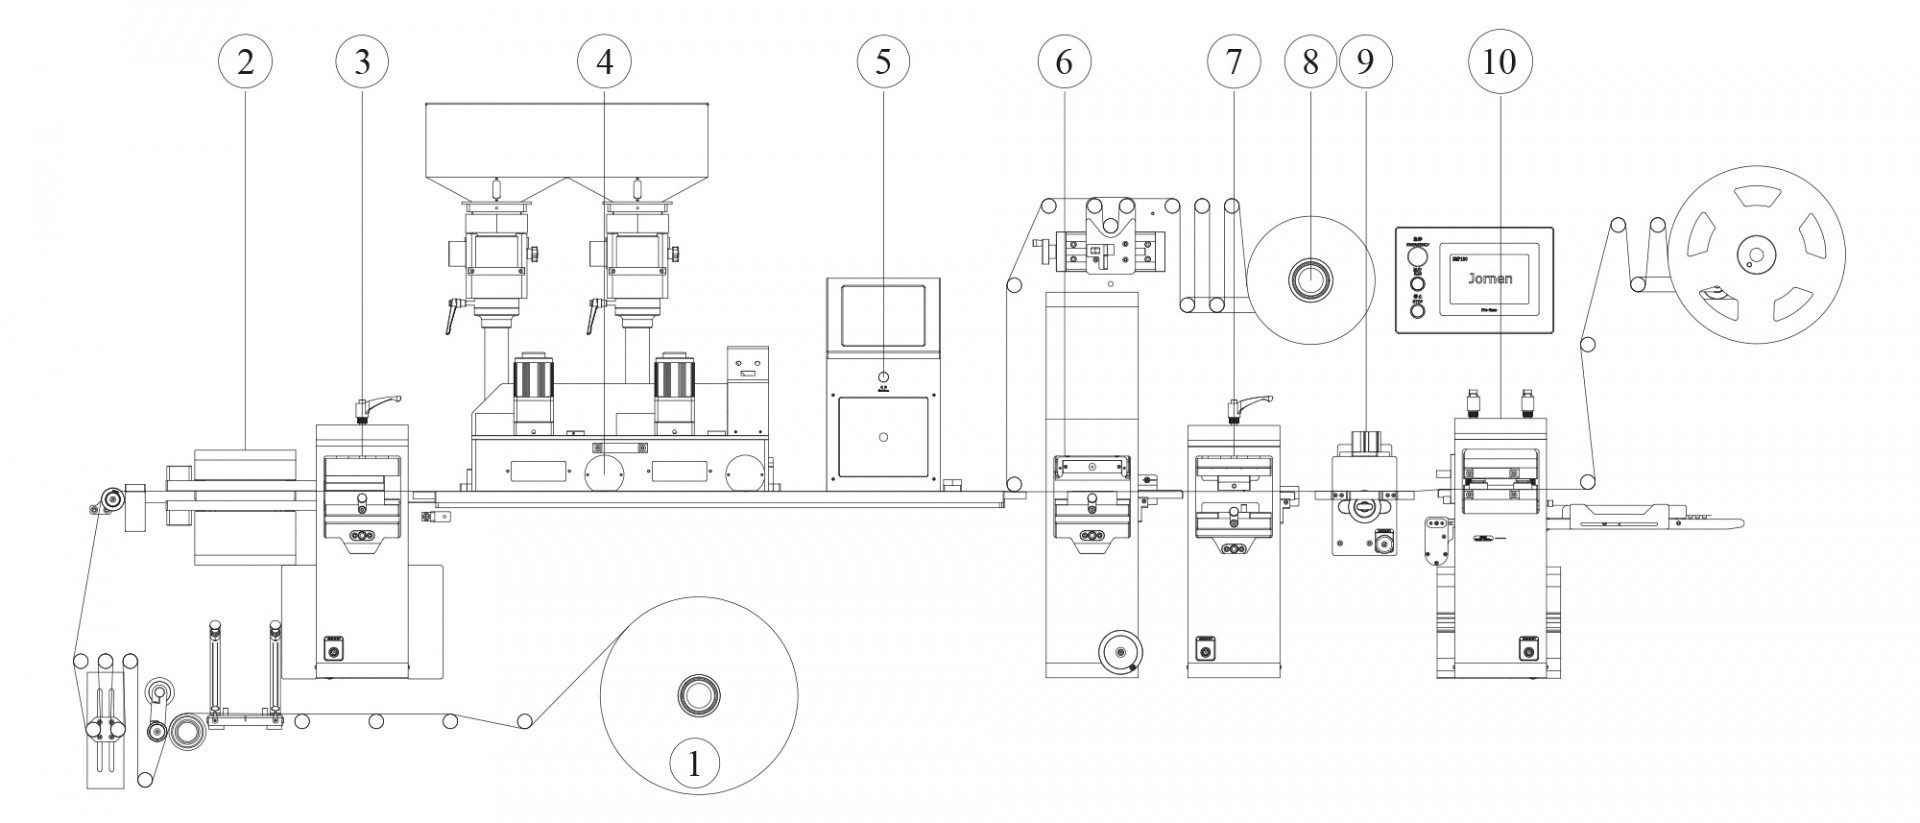
Based on their structural design, platen-type machines can be categorized by their fundamental structural layout—a critical factor that directly impacts GMP compliance, maintenance, and facility footprint.
Representing the modern standard for high-end pharmaceutical equipment, this design features a robust cantilever layout with a strict vertical partition. This architecture physically separates the machine into two distinct environments: all operational stations are cantilevered from the front of the partition, while the mechanical drive system is enclosed behind it. This strict front-to-back segregation drastically minimizes the risk of cross-contamination, ensuring that mechanical lubricants are safely kept away from the product, and pharmaceutical dust is blocked from entering the drive mechanisms. Furthermore, the open, cantilevered operating zone makes pharmaceutically compliant cleaning highly efficient and straightforward (with minimal dead corners), strongly aligning with strict cGMP principles.
In this classic configuration, the machine frame is divided vertically: the working stations are situated on top, while the mechanical drive components are housed in the cabinet below. Although physical isolation measures are implemented between the tiers, operators frequently need to adjust the horizontal positions of various stations to accommodate different product formats. These adjustments inevitably create gaps in the isolation barrier, presenting an opportunity for pharmaceutical dust or materials to fall into the lower drive compartment. Once inside, the enclosed space and complex mechanical linkages create numerous “dead corners” that make daily cleaning significantly more challenging. Despite these GMP-related drawbacks, this design remains widely utilized. Its compact overall width is highly advantageous for cleanrooms with restricted floor space, and its relatively affordable capital cost makes it a practical solution for budget-conscious manufacturing operations.
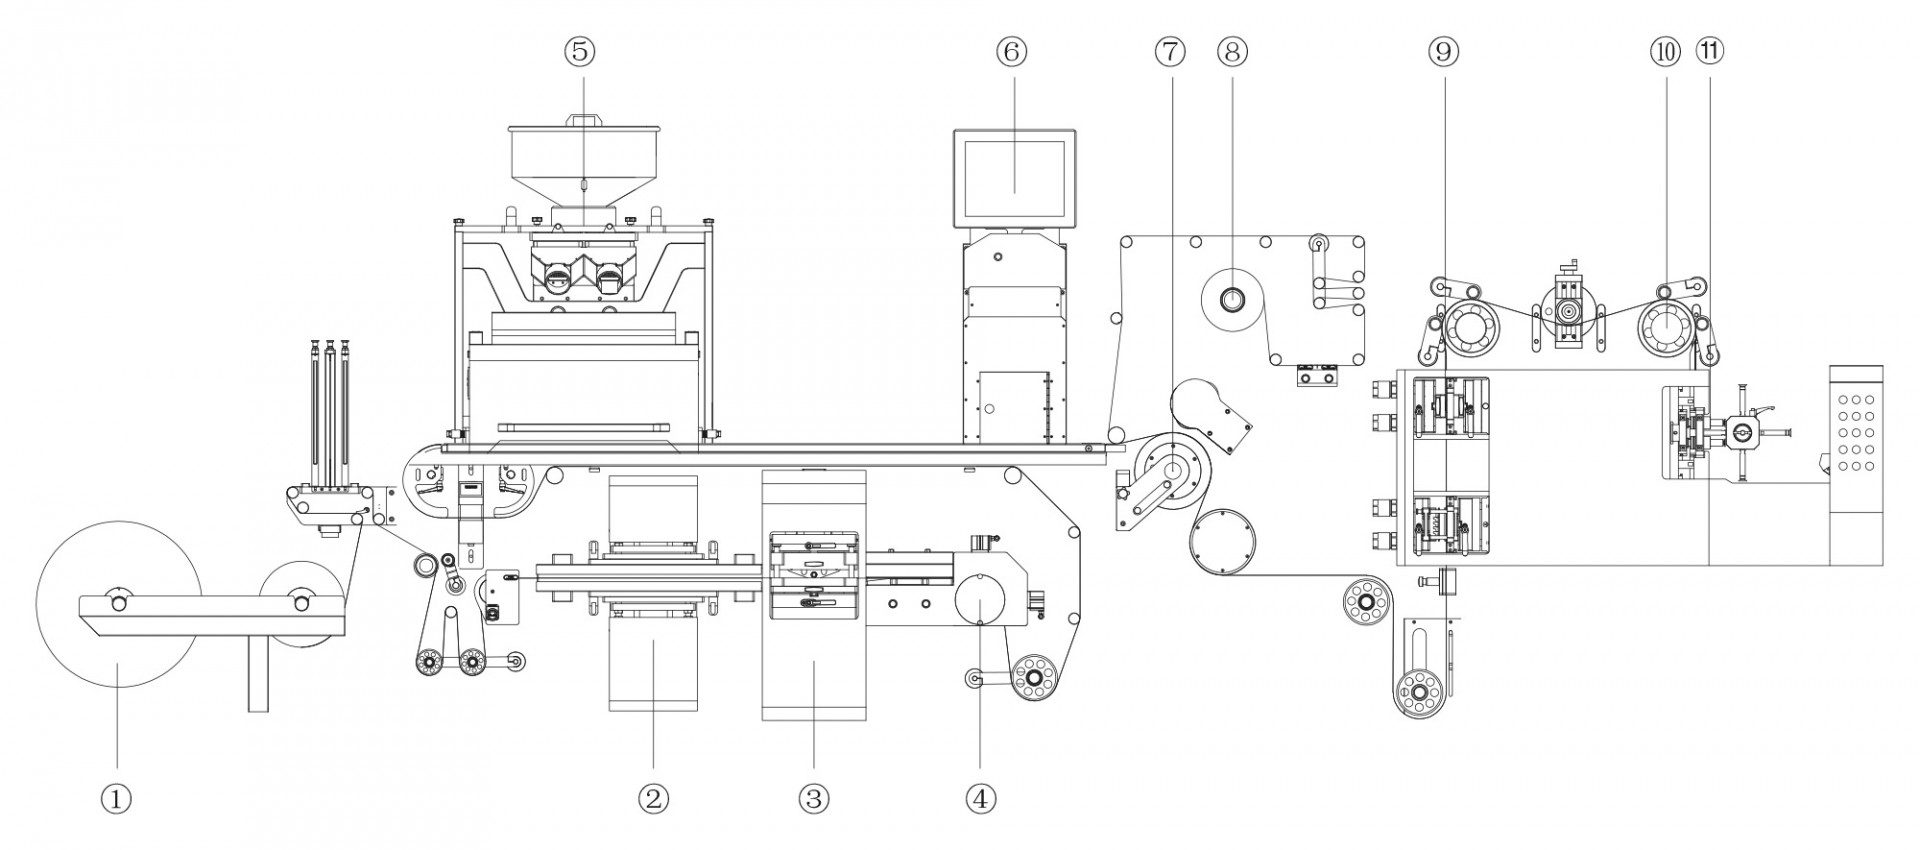
As continuous-motion rotary machines are designed for high-speed mass production, their underlying drive technology fundamentally determines their operational flexibility, especially during format changeovers.
These machines rely on a single main motor connected to a complex network of gears, timing belts, and sprockets to drive and synchronize all stations. The inherent limitation of this design becomes apparent during product changeovers, as different stations often need to operate at varying cycle ratios depending on the blister format. For example, a single stroke of the forming station might require the embossing and punching stations to cycle two, three, or even four times. To adjust these mechanical transmission ratios, operators must manually dismantle and replace physical gears or sprockets. While this rigid physical coupling is highly reliable for dedicated, single-product runs, it significantly increases both machine downtime and setup complexity.
Representing the current standard for highly flexible blister packaging, this advanced system replaces complex mechanical linkages with independent, precision-controlled servo motors at each individual station. When a change in operating ratios is required for a new blister format, operators can simply adjust the parameters directly via the PLC touch screen (HMI). This electronic synchronization completely bypasses the need for manual re-gearing, offering remarkably fast and highly convenient format changeovers. Naturally, this superior flexibility and precision require a higher initial capital investment compared to traditional mechanically driven systems.
In thermoforming, a plastic film or sheet (most commonly PVC) is heated until pliable, then shaped into blister cavities using compressed air and forming molds. For deep-draw blister cavities, relying solely on compressed air can result in excessively thin walls at the bottom of the pocket. To address this, a mechanical “plug-assist” mechanism pre-stretches the film, ensuring precise, uniform wall-thickness distribution. Additionally, this mechanical assistance allows the forming process to operate at lower temperatures, effectively preventing thermal deformation of the plastic material. Consequently, it is particularly advantageous for processing highly temperature-sensitive forming materials, such as Polypropylene (PP).
Advantages:
Disadvantages:
In cold forming, an aluminum-based laminate film is mechanically pressed into a mold using a stamp (forming plug), physically elongating the material to create and maintain the cavity shape.
Advantages:
Disadvantages:
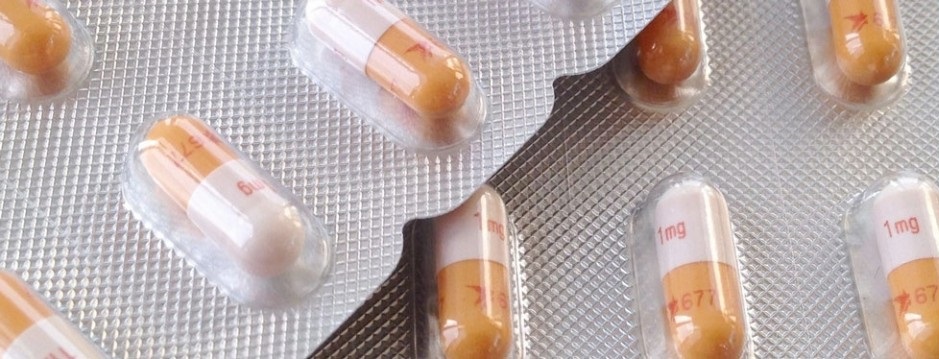
Selecting the appropriate feeding mechanism is critical. To maximize both production efficiency and overall cost-effectiveness, the feeder must be optimally matched to the specific characteristics of the solid dose.
This highly versatile feeder handles a wide array of products, including round tablets, capsules, and various irregularly shaped tablets (such as oval, capsule-shaped, and tuses a hopper, a vibratory conveyor, rotary brushes, and planetary agitators to gently sweep the products into the formed blister pockets.
The final rotary brush features denser bristles to guarantee that only correctly positioned tablets exit the feeding zone. Equipped with level-monitoring sensors and easy-to-replace brushes for quick cleaning, a major advantage of this feeder is that it requires no format parts for different product changeovers.
Specifically engineered for continuous-motion blister packaging, this feeder efficiently handles capsules and various tablet geometries (flat, oblong, and oval). The system consists of a supply hopper, a linear vibratory conveyor, a disk vibratory conveyor, and a grooved feeding plate.
The linear vibrator smoothly transfers tablets from the supply hopper to the disk vibratory conveyor. Within the disk conveyor, the tablets travel in a continuous circular motion, naturally aligning themselves into integrated guiding tracks. These tracks direct the products to drop precisely into the grooved feeding plate. Eventually, as the formed web moves continuously beneath the plate, the tablets are drawn out from the bottom of the grooves and settle accurately into the passing blister pockets.
This advanced system offers high-precision feeding and is adaptable for both intermittent and continuous-motion machines. For intermittent machines, it fills an entire index simultaneously while the web remains stationary. For continuous-motion equipment, the feeder runs reciprocally along a rail, synchronizing with the moving web to achieve full-index filling.
The feeding sequence utilizes a multi-tiered tray architecture:
In solid-dose pharmaceutical packaging, specific applications require capsules to be uniformly oriented within the blister card. This precision feature serves as a crucial anti-counterfeiting measure and significantly enhances the product’s overall aesthetic and brand consistency.
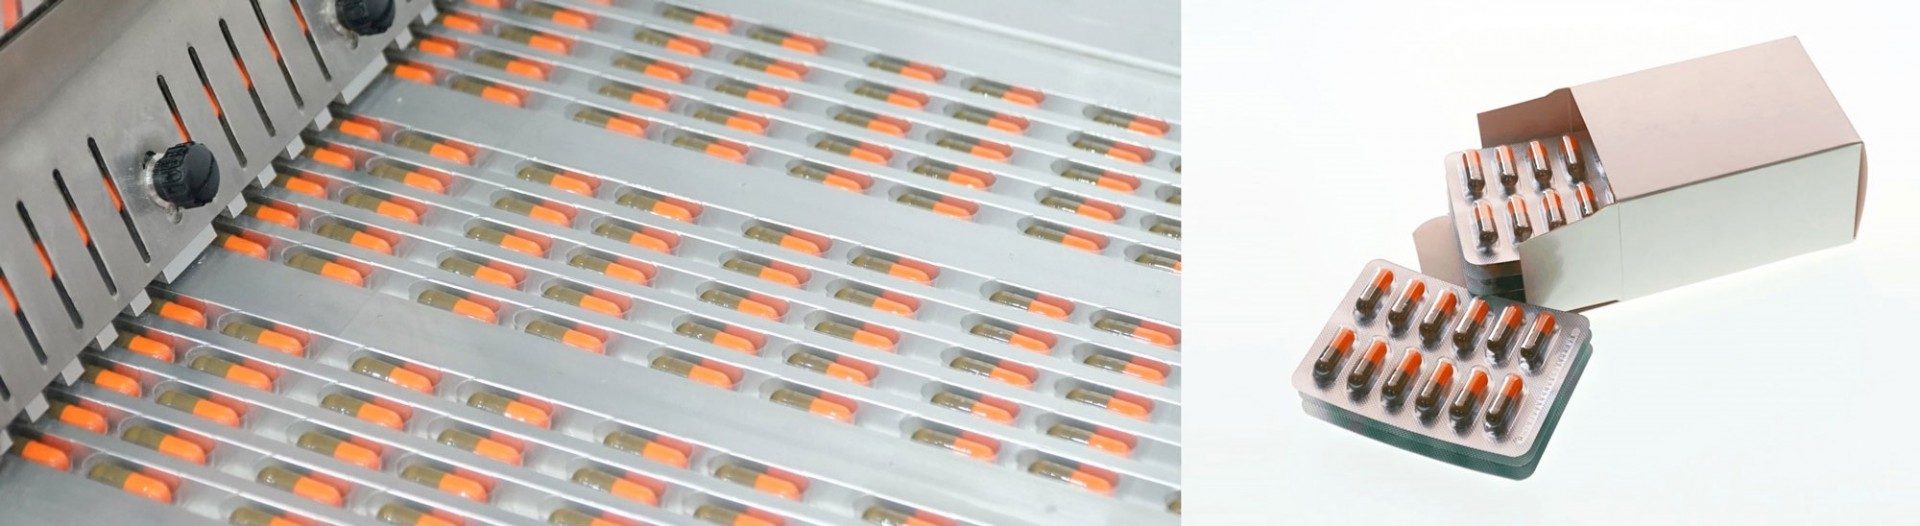
The orienting mechanism is designed to take capsules that are lying randomly in the supply hopper and automatically rectify them, aligning them all in the same direction: the cap-up position (referred to as orientation). Once oriented, the feeding device gently deposits the capsules into the blister cavities in a strictly controlled manner, ensuring perfect directional placement across the entire web.
Capsule orienting & feeding device
Handling fragile liquid containers requires extreme precision. This specialized feeder advances vials and ampoules using a synchronized combination of motor-driven rakes and a high-precision servo-driven roller.
The process begins with an infeed conveyor that smoothly transports the upright containers. A motor-driven rake then channels them into designated feeding chutes, aligning them into single-file lanes before they enter the slots of a receiving roller. Next, this servo-driven roller rotates exactly 90 degrees, carefully transitioning the vials and ampoules into a horizontal orientation. A robotic vacuum pick-and-place arm then securely grips the containers and gently deposits them into the formed web. To prevent glass breakage and ensure absolute stability during downstream transit, the blister cavities are engineered with a tailored “clamp-pack” design that firmly snaps and secures the containers in place.
Syringes—particularly pre-filled syringes (PFS) designed for rapid emergency use—require highly specialized and gentle handling.
The working principle of the syringe feeding system features:
In many clinical applications, non-pre-filled (empty) syringes are often packaged with vials and ampoules in a single, comprehensive medical kit. To produce these complex combination packs, the blister machine can be custom-engineered to integrate both the vial/ampoule feeder and the syringe feeder simultaneously.
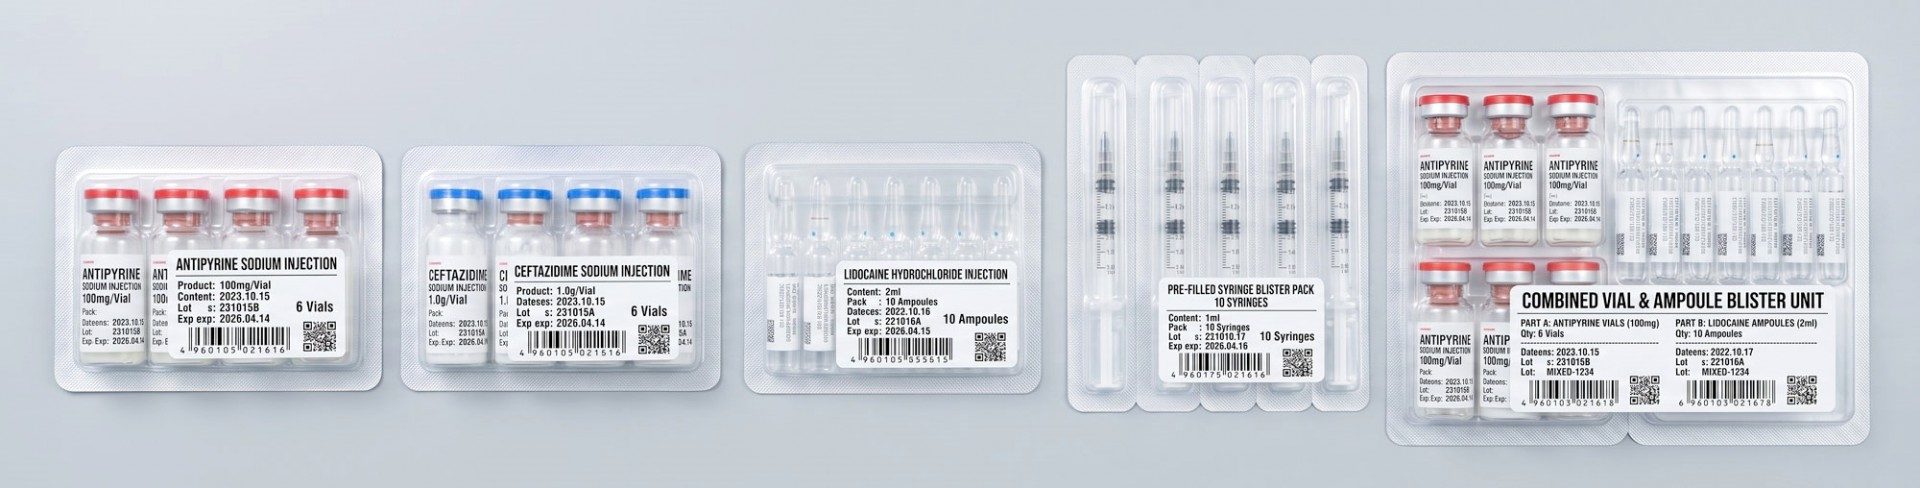
(Note: Beyond the standard configurations listed above, fully bespoke feeding systems can be custom-engineered to accommodate highly unique product characteristics and specific production requirements.)
Stringent quality control is paramount in the pharmaceutical industry, as improperly packaged products can compromise drug safety and trigger costly product recalls. To ensure flawless quality on every blister card, advanced machine vision systems (camera inspections) are seamlessly integrated into the packaging line.
To strive for zero-defect production, high-end blister machines are typically equipped with a dual-inspection configuration:
Positioned immediately after the feeding station, this first camera system inspects the open cavities to detect missing products (empty pockets), broken or chipped tablets, and deviations in product color or size.
Even if the feeding process is perfect, mechanical or alignment defects can still occur during subsequent stations. A second inspection system is employed later in the line to detect sealing wrinkles, unclear sealing grids (knurling patterns), crushed solid doses trapped in the seal, and the presence of any foreign objects. It also verifies the legibility of embossed batch numbers and detects punching misalignment (inaccurate cutting registration).
By identifying and automatically rejecting these faulty blister cards, the inspection system ensures maximum compliance and guarantees that only defect-free products reach the market.
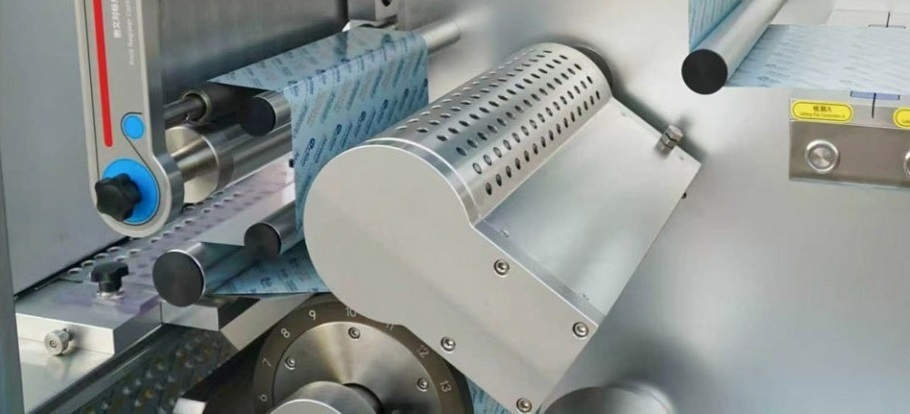
Blister sealing—the critical process of bonding the lidding foil to the formed web—is primarily executed using two distinct mechanisms: Platen-style (intermittent motion) and Rotary-style (continuous motion).
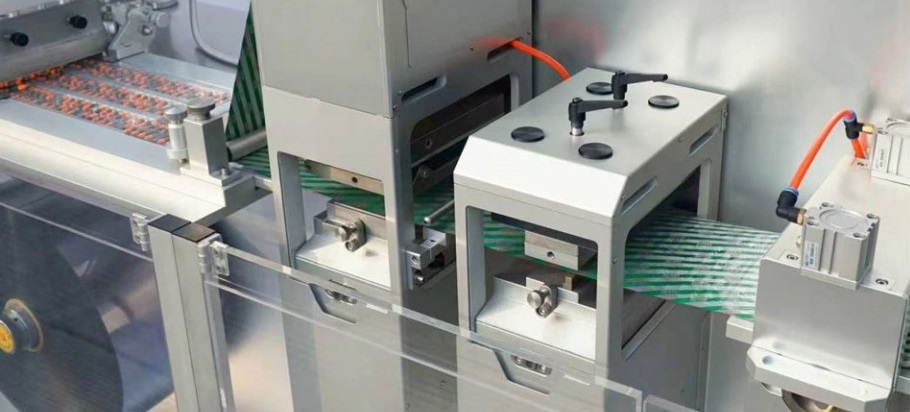
In the platen style, upper and lower flat sealing molds repeatedly close and separate to seal the blister web intermittently.
Key Advantages & Applications:
In contrast, the rotary-type utilizes a heated roller pressing against a rotating cylindrical sealing mold, continuously sealing the lidding material to the formed web via linear contact.
Key Advantages & Applications:
Considerations:
While inherently faster, the rotary-type system possesses a more complex mechanical structure. In the past, machining complex blister geometries onto a cylindrical mold was difficult. However, modern multi-axis CNC technology has completely resolved this, allowing rotary machines to easily handle various special-shaped tablets (e.g., oval, square).
Its optimal production scenario is high-volume manufacturing with relatively low format changeover frequencies (compared to the platen-type). Nevertheless, the widespread adoption of advanced servo technology has drastically simplified and accelerated modern changeovers.
Today, the true limitations of rotary sealing lie not in product shape, but in blister dimensions:
In this station, precision micro-perforations or tear-notches are applied to the web between individual pockets. This critical feature allows end-users to separate unit-doses by hand without scissors or compromising the seal integrity of the remaining units.
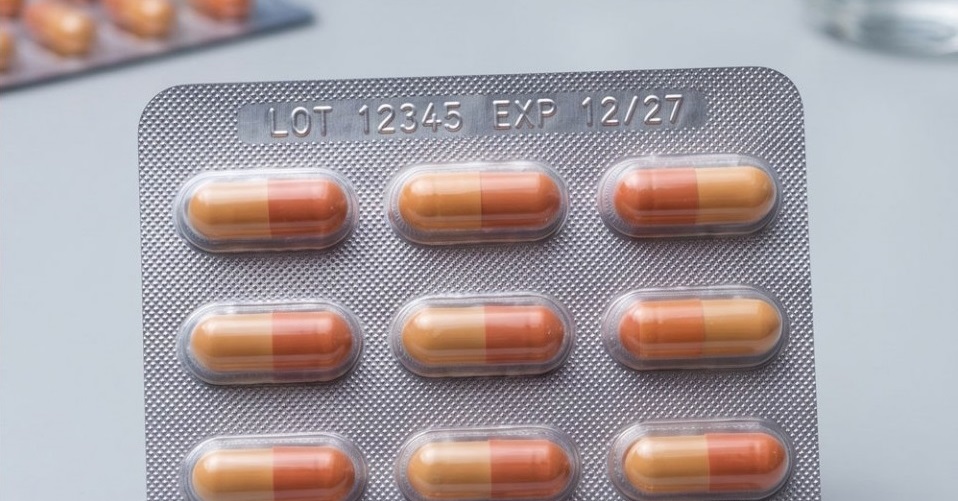
Traceability is mandatory in pharmaceutical packaging. The embossing station permanently imprints alphanumeric codes—specifically the manufacturing batch number and expiration date—into the sealed web. Depending on the machine configuration and customer requirements, these codes can be cleanly embossed onto the forming material side or directly into the lidding foil.
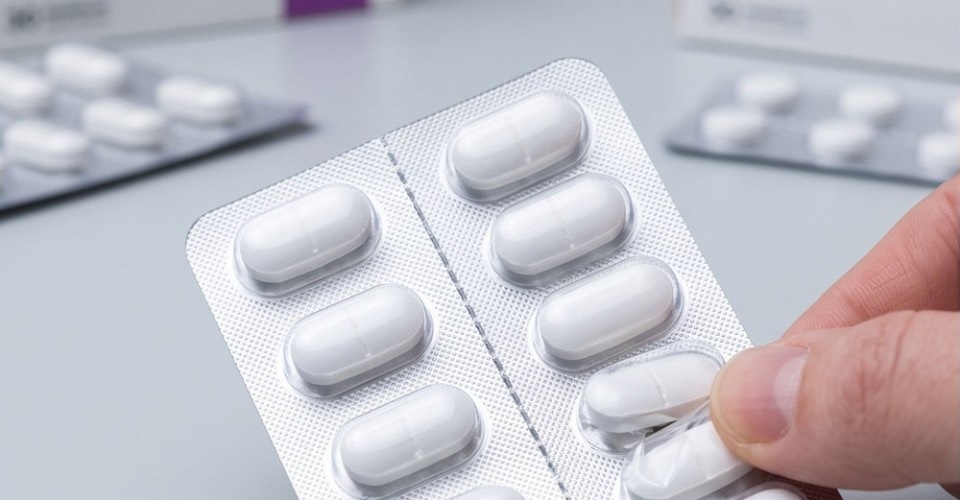
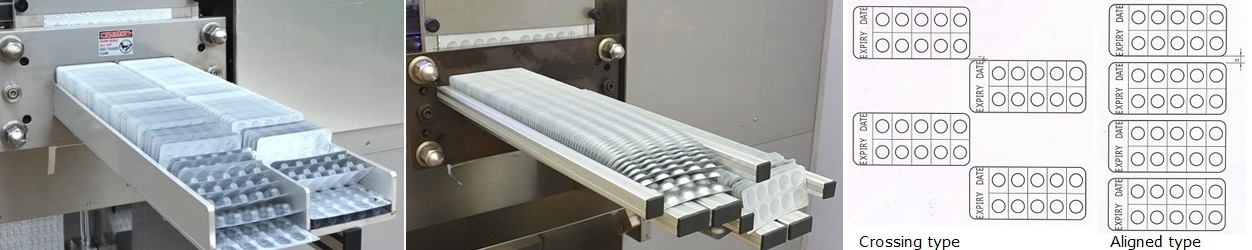
At the final punching station, individual blister cards are cleanly severed from the web by clamping the material between high-precision convex and concave dies. To optimize material consumption, tooling can be designed in two primary punching layouts:
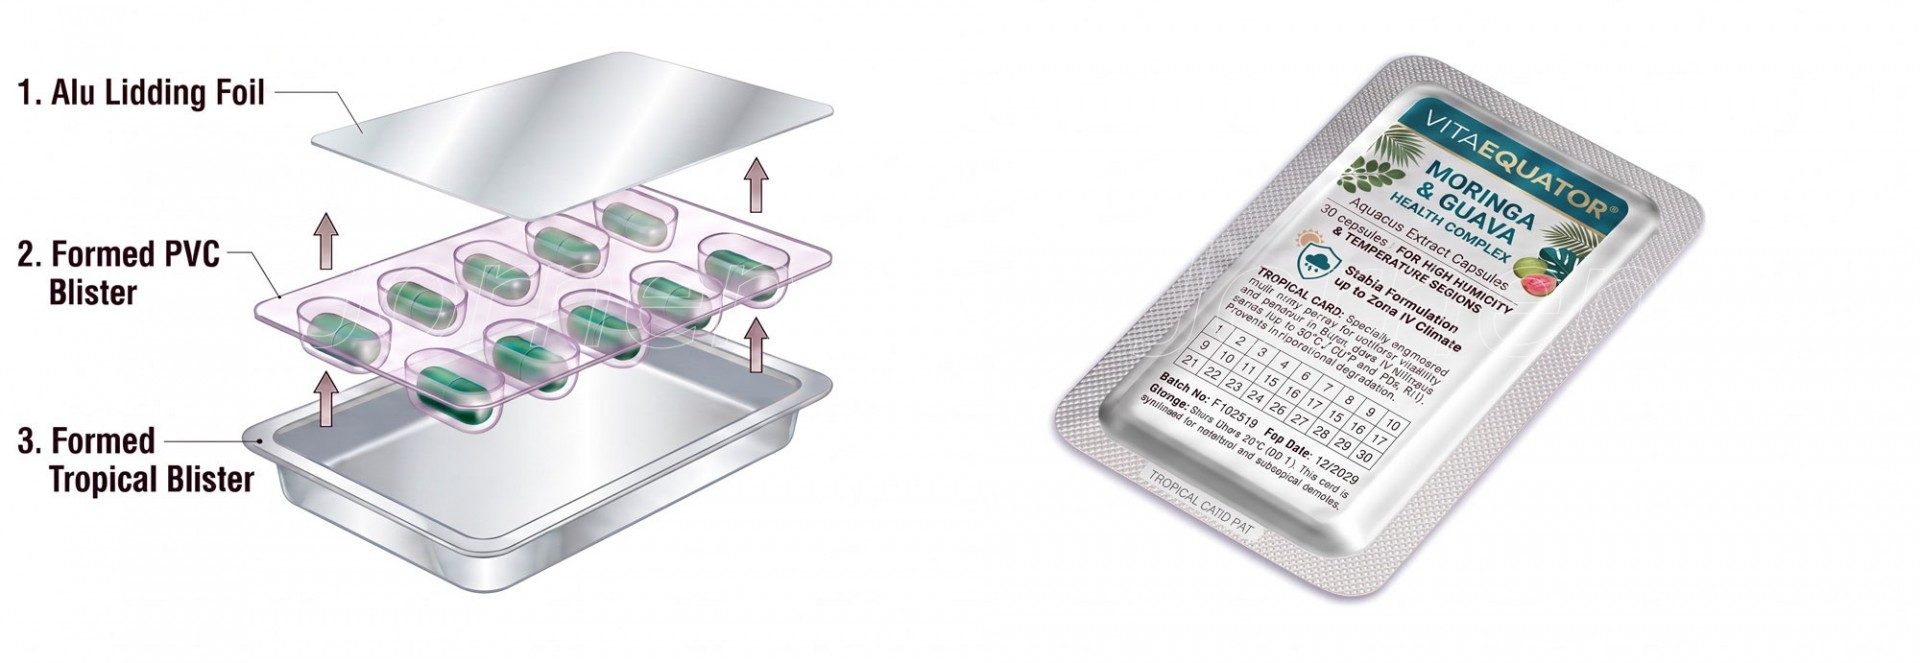
Standard blister packs typically force a compromise. Thermoformed plastic offers visual transparency (which simplifies inspection systems) and allows compact, cost-effective feeding, but it has poor moisture and oxygen barriers. Conversely, cold-formed aluminum provides ultimate protection but introduces distinct operational hurdles: its opaque nature significantly complicates machine vision inspection, and the need for larger blister footprints and complex, dedicated feeding systems dramatically increases overall costs while reducing production speed.
The Alu-PVC-Alu (often referred to as Tropical Blister) packaging machine ingeniously merges the core advantages of both forming technologies. This specialized machine integrates an additional tropical aluminum forming station and a secondary sealing station. It seals a standard thermoformed plastic blister with a protective layer of formed tropical aluminum foil. The result is a highly cost-effective, easy-to-operate package that allows for visual inspection while delivering the same near-absolute barrier protection as cold-forming.
Facility Considerations:
While highly advantageous, this dual-process capability requires a significantly extended machine footprint. Because the machine must integrate two distinct forming stations (primary thermoforming and secondary tropical aluminum) and two separate sealing stations on a single continuous line, it demands significantly more floor space. In pharmaceutical manufacturing, where ISO-certified cleanroom space is at an absolute premium, this increased machine length directly translates to higher facility overhead costs.
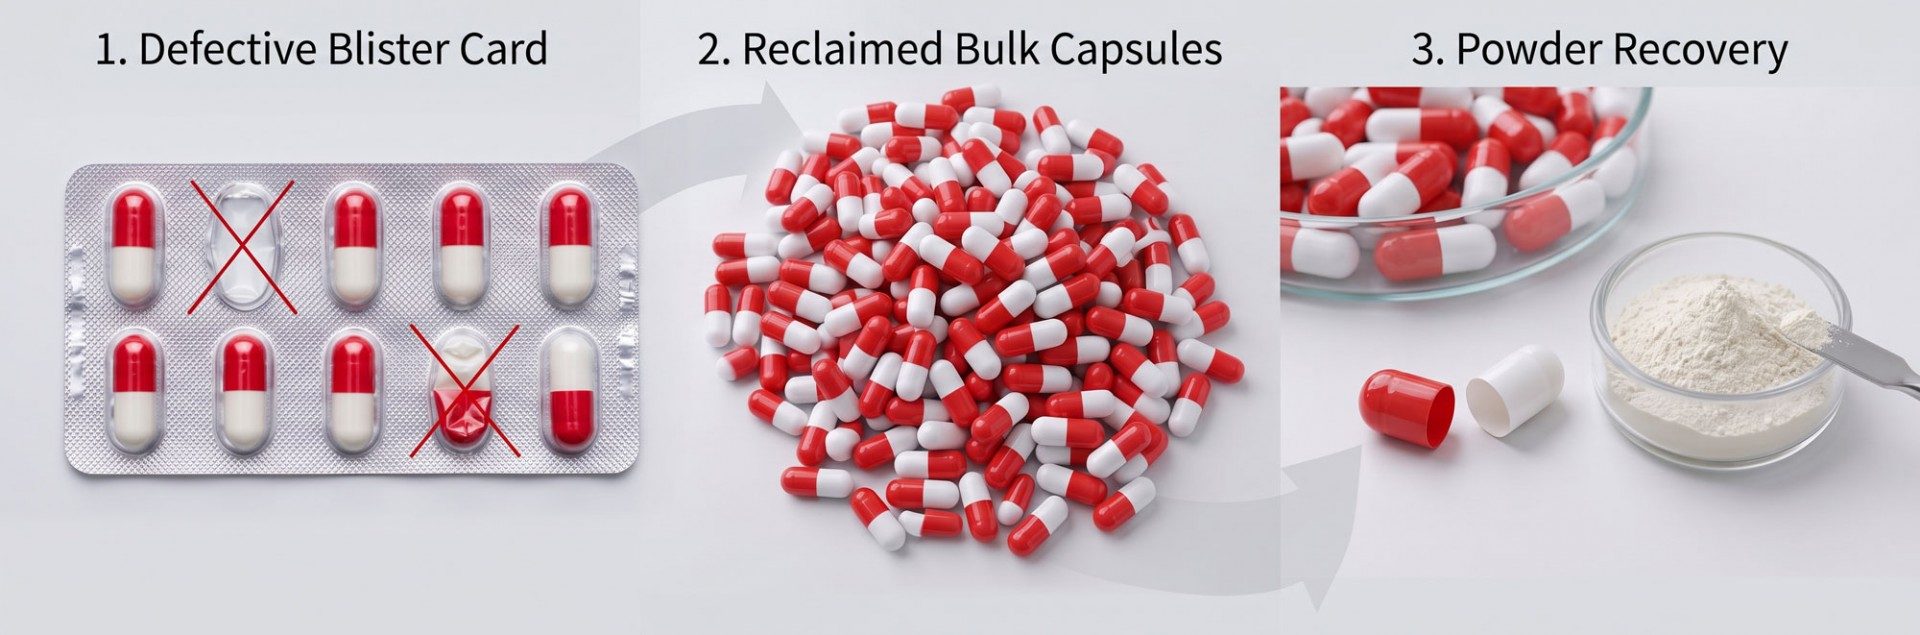
During any pharmaceutical packaging process, a certain percentage of blister cards will inevitably be rejected due to various packaging quality defects. The Deblistering Machine is a vital cost-saving accessory that safely and automatically extracts valuable tablets and capsules from these faulty packs.
To meet different production and recovery requirements, we offer two specialized product recovery systems:
Designed specifically to extract tablets or capsules from faulty blister cards. This system is highly versatile, fully adjustable, and requires zero format part changes (tool-less adjustment) for different blister sizes.
Beyond extracting capsules from rejected blister cards, this system can separate the capsules and seamlessly retrieve the internal powder or granules (applicable for capsule sizes No. 00# to 5#). This capability allows manufacturers to recycle expensive active pharmaceutical ingredients (APIs) and drastically reduce production waste.
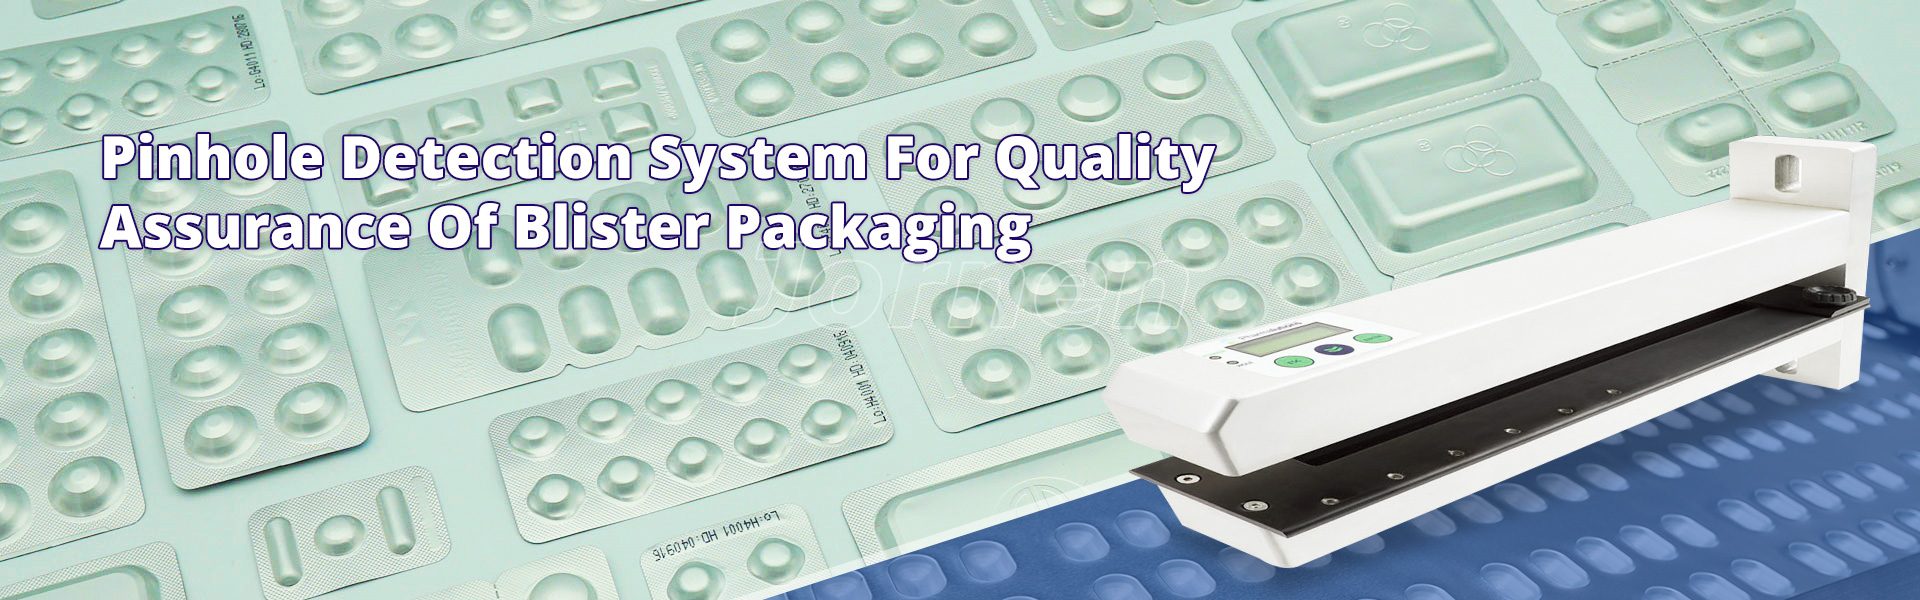
While cold-formed Alu-Alu blisters offer superior barrier protection, the intense mechanical elongation process can sometimes cause microscopic pinholes, pores, or micro-fractures in the aluminum film—defects that lead to drug oxidation but are invisible to the naked eye.
To guarantee uncompromised drug safety, installing an inline pinhole detector is critical. This system utilizes a highly sensitive far-infrared light emitter and receiver spanning the entire width of the cold-formed film. If it detects light penetrating through microscopic fractures—whether caused by improper mold design, over-stretching, or defective raw materials—the system instantly triggers a visual alarm. The machine’s control system then halts feeding into that faulty segment and automatically rejects the compromised blister card after the punching station.
Selecting the correct forming material is paramount, as it directly determines the final package’s barrier protection level.
The traditional industry standard. It is highly cost-effective and exceptionally easy to thermoform. However, it offers relatively poor barrier properties against moisture and oxygen, making it unsuitable for highly sensitive drugs. Furthermore, its chlorine content presents growing environmental disposal concerns.
Typically applied as a coating over PVC, PVDC achieves significantly higher barrier properties depending on the coating thickness. It is highly favored in pharmaceuticals for its excellent moisture resistance. However, the film is more expensive and releases harmful hydrogen chloride gas if incinerated.
A modern, highly eco-friendly alternative. While offering a baseline barrier profile comparable to standard PVC, it is halogen-free and burns cleanly without releasing highly toxic, corrosive gases (such as HCl). Additionally, due to its lower density, PP yields more blisters per kilogram than PVC.
The pharmaceutical industry is currently experiencing a major shift toward using PP for both the forming web and the lidding material. Traditional blister packs are notoriously difficult to recycle because the aluminum foil is heat-sealed to the PVC base and cannot be easily separated. By using PP for both structural components—the forming web and the lidding material—manufacturers create a true “mono-material” package. This eliminates the need for separation, making the entire blister pack 100% recyclable.
PP is extremely sensitive to thermal fluctuations, exhibiting significant deformation and high shrinkage at elevated temperatures. Processing PP requires heavily modified, precision-controlled thermoforming stations to accommodate its unique shrinkage characteristics. To mitigate these issues, modern equipment engineering focuses on two critical upgrades:
Provides the ultimate barrier. However, as discussed, it is prone to micro-fractures (requiring inline pinhole detectors) and demands a larger cavity footprint and dedicated feeding mechanisms, all of which significantly drive up overall production costs. Furthermore, it presents a major sustainability challenge: cold-form foil is a complex multi-material laminate (typically OPA/Alu/PVC), making layer separation and recycling notoriously difficult.
The pharmaceutical packaging landscape is continuously evolving. Driven by rapid advancements in polymer science and stricter environmental regulations, the industry will continue to see the emergence of next-generation materials. These future substrates will be engineered to deliver the ultimate balance: uncompromised barrier performance, optimal machinability, and full lifecycle sustainability, seamlessly adapting to the ever-changing demands of global pharmaceutical manufacturing.
Equipment selection is dictated by production scale, facility layout constraints, and specific solid dose barrier requirements. The following matrix outlines the primary blister machine architectures.
(Note: Unless otherwise specified, all maximum output capacities referenced below assume optimal feeding conditions with no restriction on product infeed. Calculations are strictly based on standard Alu-PVC thermoforming processes utilizing a 57×80mm blister card format.)
Small to Medium Batches
Platen-style machines utilize intermittent motion for forming and sealing, providing extended dwell times suitable for varied blister formats and rapid changeovers.
Recommended Series: JORNEN BMP Balcony Blister Machines
The BMP series features a cGMP-compliant cantilever architecture that physically segregates the drive mechanisms from the operating zone to mitigate cross-contamination risks.
Engineered for laboratory scale and R&D applications. Maximum web width: 100mm. Output: Up to 25 blisters/min.
Designed for low-volume commercial production with a compact footprint. Maximum web width: 180mm. Output: Up to 150 blisters/min.
Medium-capacity system. Maximum web width: 270mm. Output: Up to 200 blisters/min.
High-Speed Mass Production
Rotary sealing technology provides continuous web movement, eliminating intermittent indexing stops. This architecture is mandatory for dedicated, high-volume production lines.
Recommended Series: JORNEN BMR & DPH Blister Machines
These systems integrate multi-axis servo drives to synchronize continuous sealing with formatting stations, reducing mechanical wear at high operational speeds.
High-speed continuous sealing. Output: Up to 400 blisters/min.
Flagship rotary model. Maximum web width: 270mm. Output: Up to 600 blisters/min.
Ultra-high volume industrial platform. Features a 390mm web width. Output: Up to 800 blisters/min (calculated on a 57×90mm blister format). Available in full-servo or mechanical transmission configurations.
For cleanroom facilities with strict space limitations where the cantilever design is not a primary requirement, traditional top-to-bottom architectures provide an economical and highly compact solution.
Recommended Series: JORNEN DPP Traditional Platen Machines
The DPP series utilizes a vertical structural division, housing drive components in the lower cabinet to minimize the machine’s overall width.
Compact platen machine. Web width: 150mm. Output: Up to 100 blisters/min.
Standard economical production unit. Output: Up to 200 blisters/min. (Extended web widths available: DPP350 and DPP500).
When formulations demand the absolute barrier protection of cold-formed Alu-Alu but operational parameters require the efficiency of thermoforming, the tropical blister architecture is the standard solution. This dual-forming process utilizes transparent PVC for the primary cavity, enabling reliable camera inspection and the use of standard universal feeders. It maintains compact blister card dimensions while applying a secondary cold-formed tropical aluminum layer to establish an impermeable barrier against moisture and light. To accommodate varying production scales, the JORNEN tropical blister series offers two primary configurations: the Tropical Blister Machine DPH390H3 for high-volume operations and the Tropical Blister Machine DPP260H3 for medium-capacity requirements.